minghungmachinery@gmail.com   ▏           +8618769900191 / +8615589105786

PRODUCT CATEGORY

Knife Grinder Instruction Book

Knife Sharpener Operation Manual
1. Select the appropriate grinding wheel according to the material of the grinding tool, generally grind the HS-CO NACHI milling cutter. The SG-FAX milling cutter uses a white grinding wheel with an inner hole of 20mm of 80K. If grinding tungsten steel, a diamond grinding wheel must be used;
2. Retract the grinding wheel feed fine-tuning nut (1) inward until it is aligned with the small hole of the spindle. After alignment, insert the fixing pin (6) into the hole so that the grinding wheel spindle cannot rotate, and the groove of the gasket faces inward. , and close to the grinding wheel surface, use the dismantling aluminum wrench to lock the nut;
3. After the grinding wheel is clamped on the grinding wheel spindle, pull out the fixed pin (6), and use the diamond dresser (8) to dress the grinding wheel. When dressing the grinding wheel, do not dress too much at one time to avoid the diamond falling;
4. Adjust the rotation tightness of the spindle. When the spindle seat rotates 90°, if the upper and lower clearance is too large, you can use two wrenches to loosen the nuts in opposite directions, and then adjust to the proper tightness one by one.
5. Adjustment of the 0° angle of the main shaft seat: Use a 10mm hex wrench to adjust the stop bolt (19) under the 90° indexing plate to be movable, loosen the 90° lock nut (18), and pull up the 90° index Disc fixing bolt (14). Use a 12mm round bar to grind about 60mm long. If the front end size is larger than the rear end size, adjust the wrench to the left and adjust it according to the size. If the front end size of the grinding size is smaller than the rear end size, then Adjust the wrench to the left until the front and rear dimensions are the same;
6. Adjust the spindle seat 90° with a 5mm wrench at the inner corner to adjust the stop bolt (19), clamp the Φ12mm round bar on the upper end face of the spindle seat and align the grinding wheel surface, fix the spindle seat at the 90° position and shake the spindle seat in an arc up and down. , Apply the blue dan to the end face of the round bar. If the right side of the end face is ground first, it means that 90° is over; The end face can be ground up to the left and right. When adjusting, the 90° fixing nut and the 90° indexing plate fixing bolt (14) must be loosened. When the adjustment is complete, the 90° indexing plate can be reset to zero and fixed with T6 fixing bolts;
7. Select a suitable sleeve according to the diameter of the grinding mill shank, clamp the shank on the spindle seat, and lock the nut (11) behind the spindle seat;
8. According to the shape of the grinding tool, adjust the angles on the spindle seat and lock the corresponding nuts;
9. When grinding is not started, the tool and the grinding wheel should keep a distance not too close to prevent the grinding wheel and the tool from colliding when the machine is turned on;
10. Turn on the grinder switch (2), let the grinding wheel rotate for more than 1 minute, and then start grinding after confirming that there is no abnormal phenomenon;
11. Turn the sleeve lock nut (11) with your right hand, and adjust the feed fine-tuning nut (1) with your left hand. When the grinding wheel is about to touch the tool,
The knife should be fed slowly to avoid bumping the grinding wheel;
12. The amount of feed should be matched with the rotation of the tool bar, and the amount of feed should not be too large, so as not to burn the tool and cause annealing;
 
Availability:
Quantity:
sharethis sharing button
  • MH-KG3200A

  • MINGHUNG

  • Qingdao, China

  • L/C, T/T

  • two years

SHANDONG MINGHUNG WOOD MACHINERY CO.,LTD

INSTRUCTION KNIFE GRINDER               

Contact: 0086 18769900191

Website:  www.plywoodmachineline.com

Email: minghungmachinery@gmail.com

SHANDONG MINGHUNG WOOD MACHINERY CO.,LTD


Knife Sharpener Operation Manual
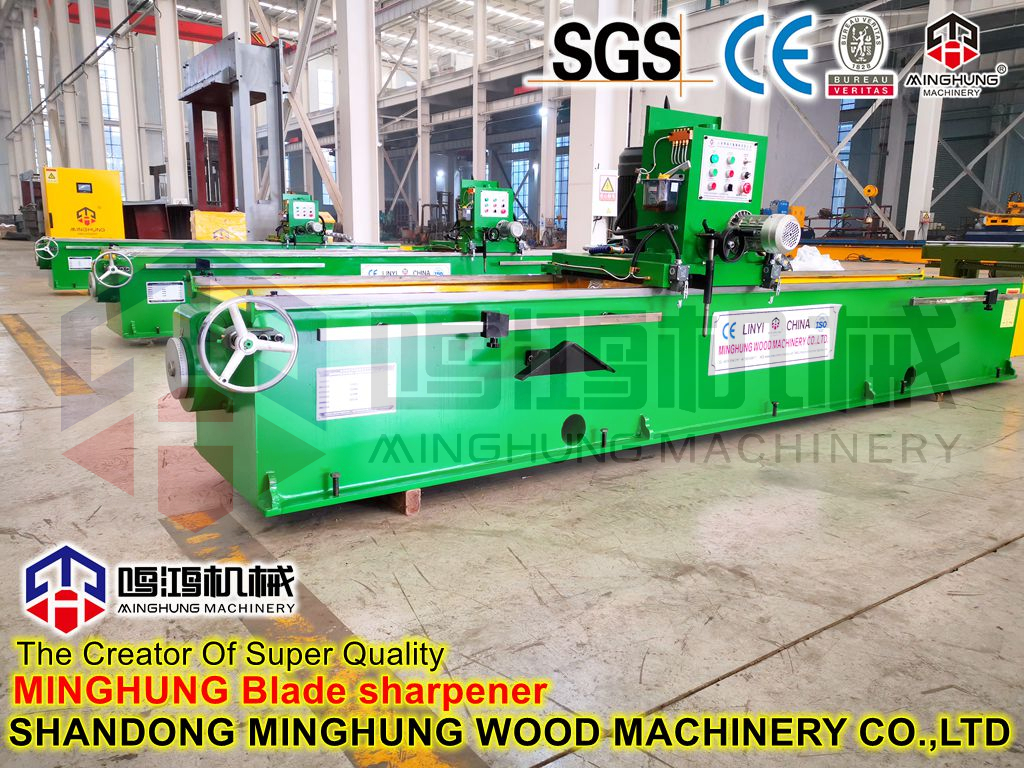
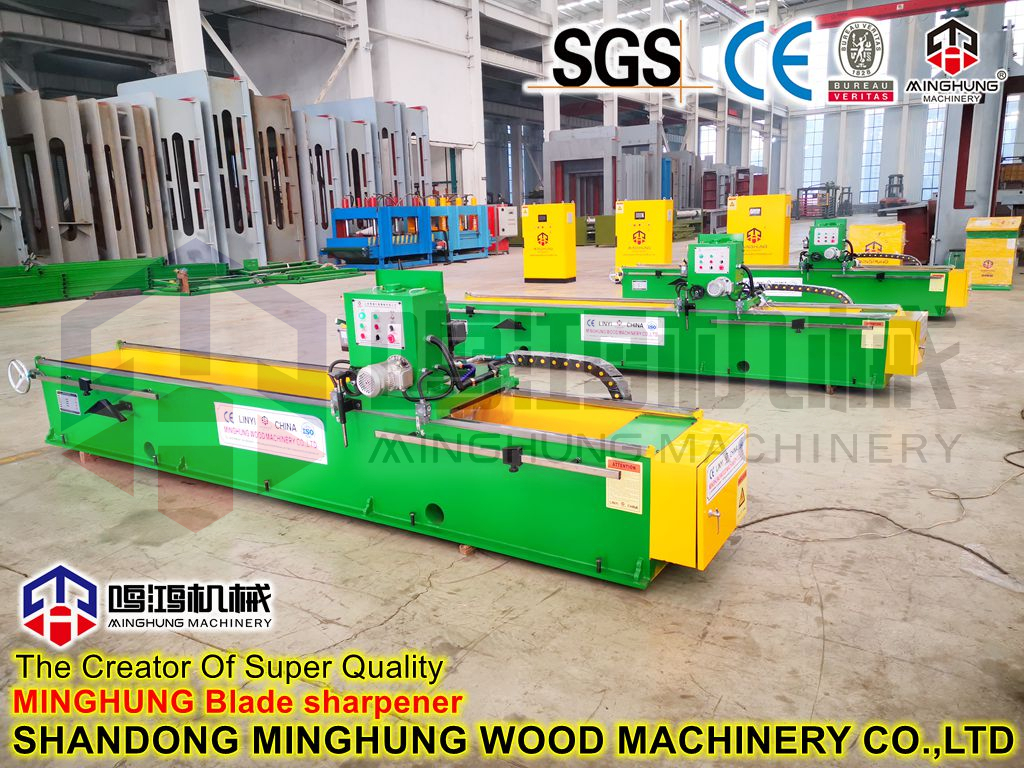
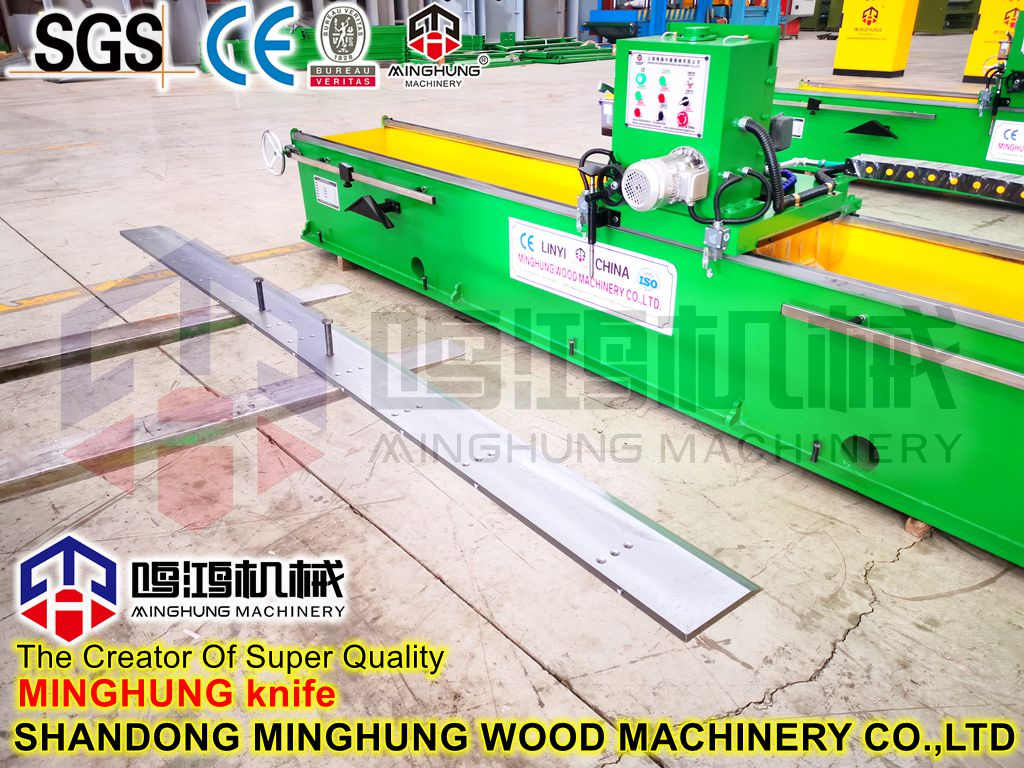
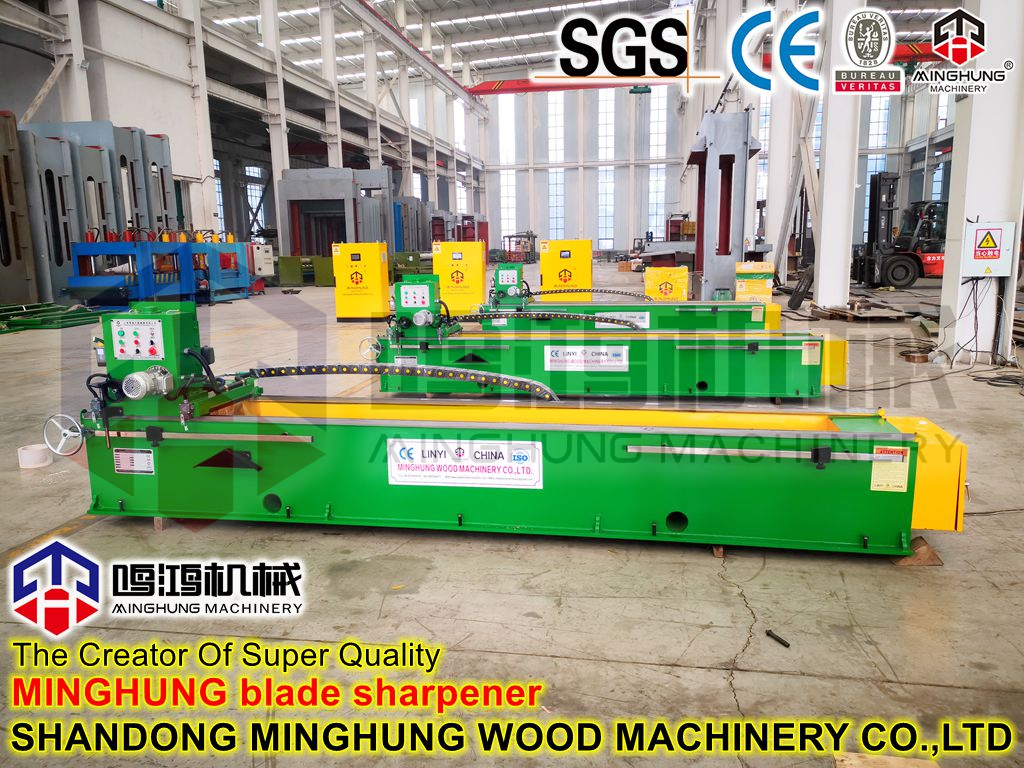
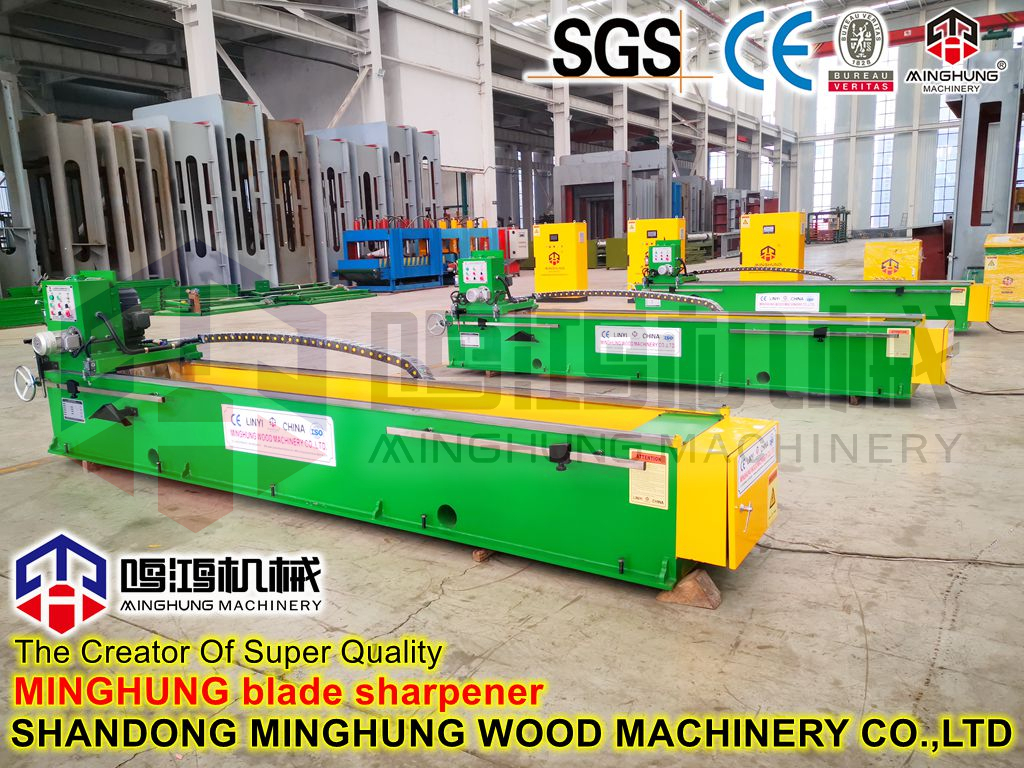
Blade sharpener from MINGHUNG machineBlade sharpenerminghung knife


1. Select the appropriate grinding wheel according to the material of the grinding tool, generally grind the HS-CO NACHI milling cutter. The SG-FAX milling cutter uses a white grinding wheel with an inner hole of 20mm of 80K. If grinding tungsten steel, a diamond grinding wheel must be used;
2. Retract the grinding wheel feed fine-tuning nut (1) inward until it is aligned with the small hole of the spindle. After alignment, insert the fixing pin (6) into the hole so that the grinding wheel spindle cannot rotate, and the groove of the gasket faces inward. , and close to the grinding wheel surface, use the dismantling aluminum wrench to lock the nut;
3. After the grinding wheel is clamped on the grinding wheel spindle, pull out the fixed pin (6), and use the diamond dresser (8) to dress the grinding wheel. When dressing the grinding wheel, do not dress too much at one time to avoid the diamond falling;
4. Adjust the rotation tightness of the spindle. When the spindle seat rotates 90°, if the upper and lower clearance is too large, you can use two wrenches to loosen the nuts in opposite directions, and then adjust to the proper tightness one by one.
5. Adjustment of the 0° angle of the main shaft seat: Use a 10mm hex wrench to adjust the stop bolt (19) under the 90° indexing plate to be movable, loosen the 90° lock nut (18), and pull up the 90° index Disc fixing bolt (14). Use a 12mm round bar to grind about 60mm long. If the front end size is larger than the rear end size, adjust the wrench to the left and adjust it according to the size. If the front end size of the grinding size is smaller than the rear end size, then Adjust the wrench to the left until the front and rear dimensions are the same;
6. Adjust the spindle seat 90° with a 5mm wrench at the inner corner to adjust the stop bolt (19), clamp the Φ12mm round bar on the upper end face of the spindle seat and align the grinding wheel surface, fix the spindle seat at the 90° position and shake the spindle seat in an arc up and down. , Apply the blue dan to the end face of the round bar. If the right side of the end face is ground first, it means that 90° is over; The end face can be ground up to the left and right. When adjusting, the 90° fixing nut and the 90° indexing plate fixing bolt (14) must be loosened. When the adjustment is complete, the 90° indexing plate can be reset to zero and fixed with T6 fixing bolts;
7. Select a suitable sleeve according to the diameter of the grinding mill shank, clamp the shank on the spindle seat, and lock the nut (11) behind the spindle seat;
8. According to the shape of the grinding tool, adjust the angles on the spindle seat and lock the corresponding nuts;
9. When grinding is not started, the tool and the grinding wheel should keep a distance not too close to prevent the grinding wheel and the tool from colliding when the machine is turned on;
10. Turn on the grinder switch (2), let the grinding wheel rotate for more than 1 minute, and then start grinding after confirming that there is no abnormal phenomenon;
11. Turn the sleeve lock nut (11) with your right hand, and adjust the feed fine-tuning nut (1) with your left hand. When the grinding wheel is about to touch the tool,
The knife should be fed slowly to avoid bumping the grinding wheel;
12. The amount of feed should be matched with the rotation of the tool bar, and the amount of feed should not be too large, so as not to burn the tool and cause annealing;

Previous: 
Next: 
Product Inquiry
Fair hall01_614_614.png
Shanghai International Woodworking Machinery Fair Day 1 Report: Overwhelming Popularity!
09-08 2026

The first day of the 2026 Shanghai International Woodworking Machinery Fair – if this morning's keyword was "surprise," then this afternoon's keywords are definitely "explosive" and "confidence"!

Read More
Fair hall11_614_614.png
The 2026 Shanghai International Woodworking Machinery Exhibition Came To A Perfect Close — We Reaped A Bountiful Harvest!
09-11 2026

This trip to Shanghai was not only a display of products, but also a dissemination of our brand and a connection of emotions. We will continue to stay true to our original aspiration and repay every customer's trust and support with even better products and services. The future is full of promise, and we are always on the way!

Read More
plywood machine deliver (8)_649_649.png
The Moon Grows Full, But No One Rests — The Dedication Behind 25 Containers
09-29 2026

The Mid-Autumn Festival is approaching, and the moon is growing round. While many people are beginning to prepare for family reunions, the company’s factory tells a different story: forklifts weaving through the yard, crane arms rising and falling, containers lined up in rows, and loading work proceeding in a tense yet orderly manner.

Read More
Particleboard paving machine.jpg
How to produce Particle board? What is the production step
09-09 2023

How to produce Particle board? What is the production step of Making Particle board?Introduction:Particle board, also known as chipboard, is a versatile and cost-effective material widely used in the construction and furniture industries. It is made by compressing wood particles and adhesive togethe

Read More
车间3_副本.png
A New Chapter in Smart Manufacturing: Our 18-Month Journey To A Brand-New Facility
07-29 2026

This new facility marks a fresh start for our company. Guided by our enduring commitment to "precision engineering and quality first," we are now better equipped than ever to provide efficient, durable, and innovative machinery solutions for the worldwide wood-based panel industry.

Read More
Shandong MINGHUNG Wood Machinery Co.,Ltd is one famous manufacturer of plywood machine in China, located in Linyi city. 
Home

PRODUCT GROUPS

CONTACT US

 +86-18769900191 /  +86-15589105786 
 +86-18769900191 / +86-15589105786
 
minghungmachinery@gmail.com
  Fangcheng Town,Lanshan District,Linyi City,Shandong Province,China
Copyright © 2010 SHANDONG MINGHUNG WOOD MACHINERY CO.,LTD