Furniture-Grade Eco Plywood System
|
Main Production Equipment in the line
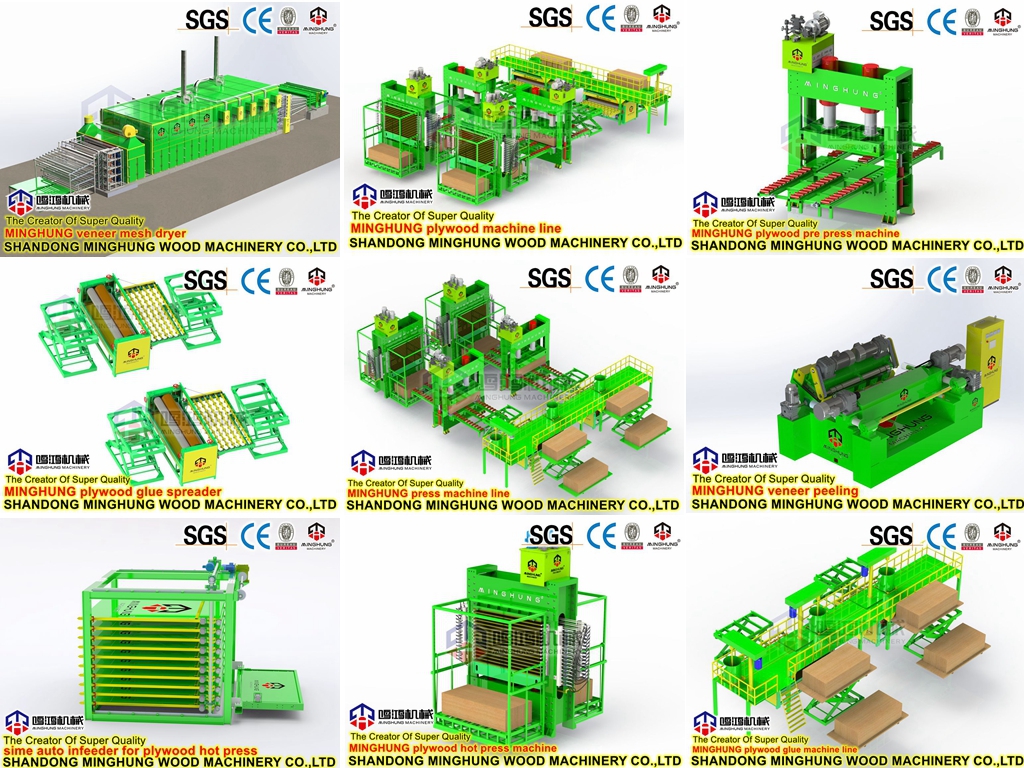
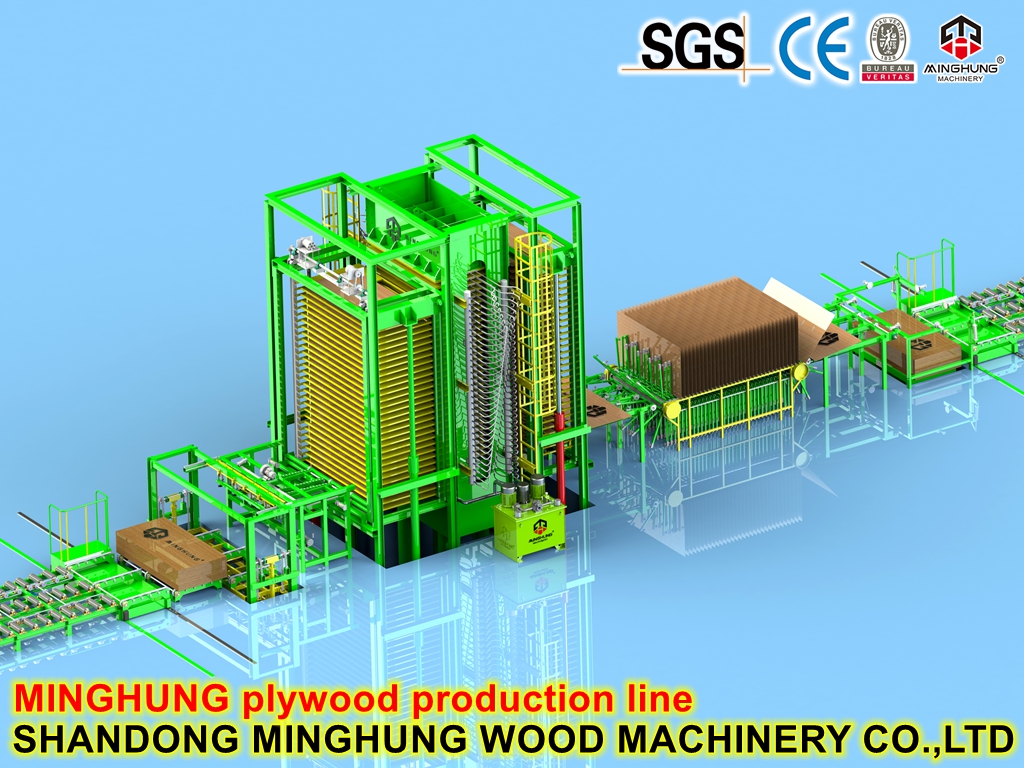
A complete continuous production line for furniture-grade eco-friendly plywood primarily includes the following core equipment:
1. Log Processing Line: Includes log saw, debarker, hot water bath, etc.
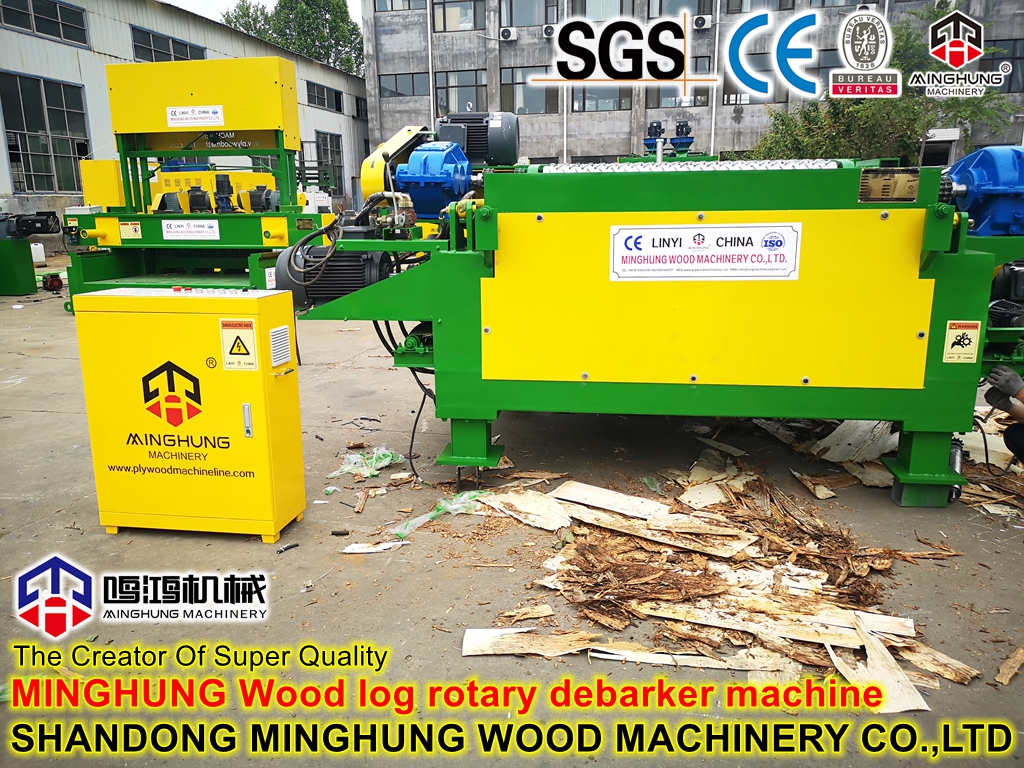
debarker
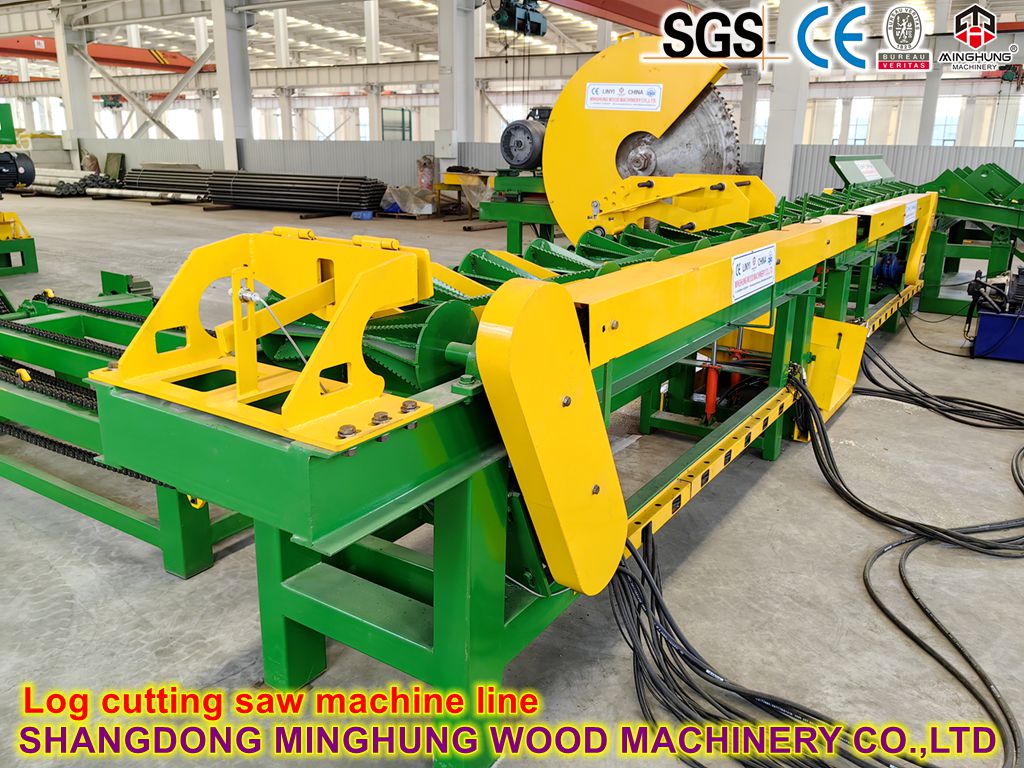
cutting saw
2. Veneer Lathe (Peeler): The core equipment that peels logs into continuous veneer.
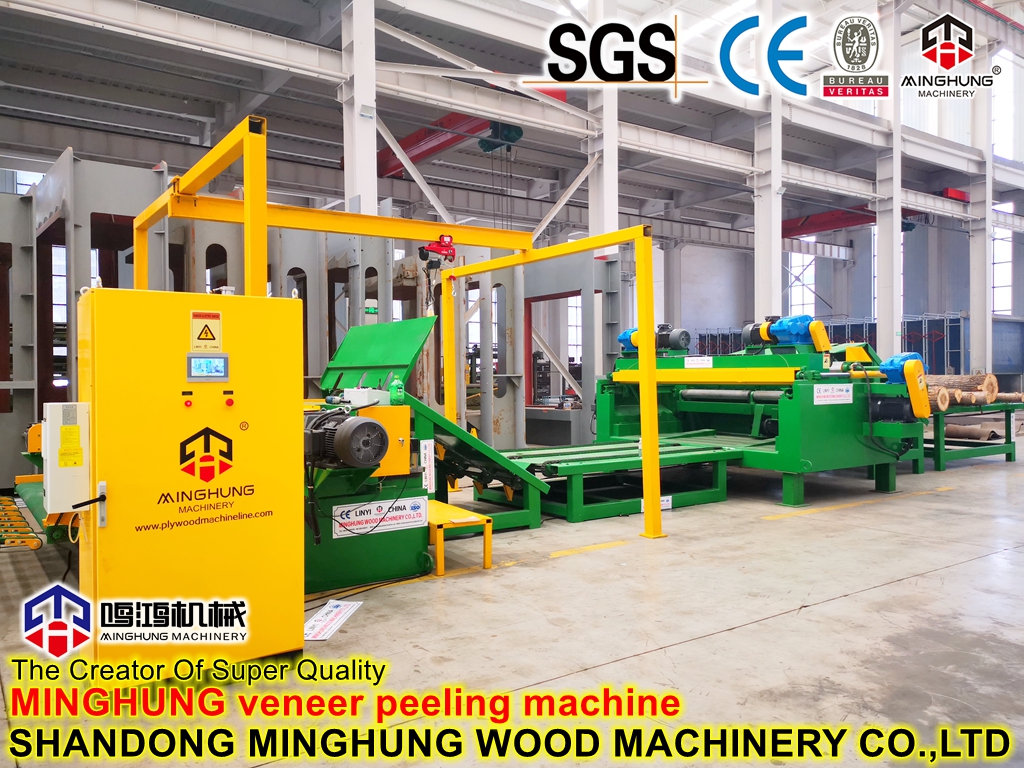
veneer lathe
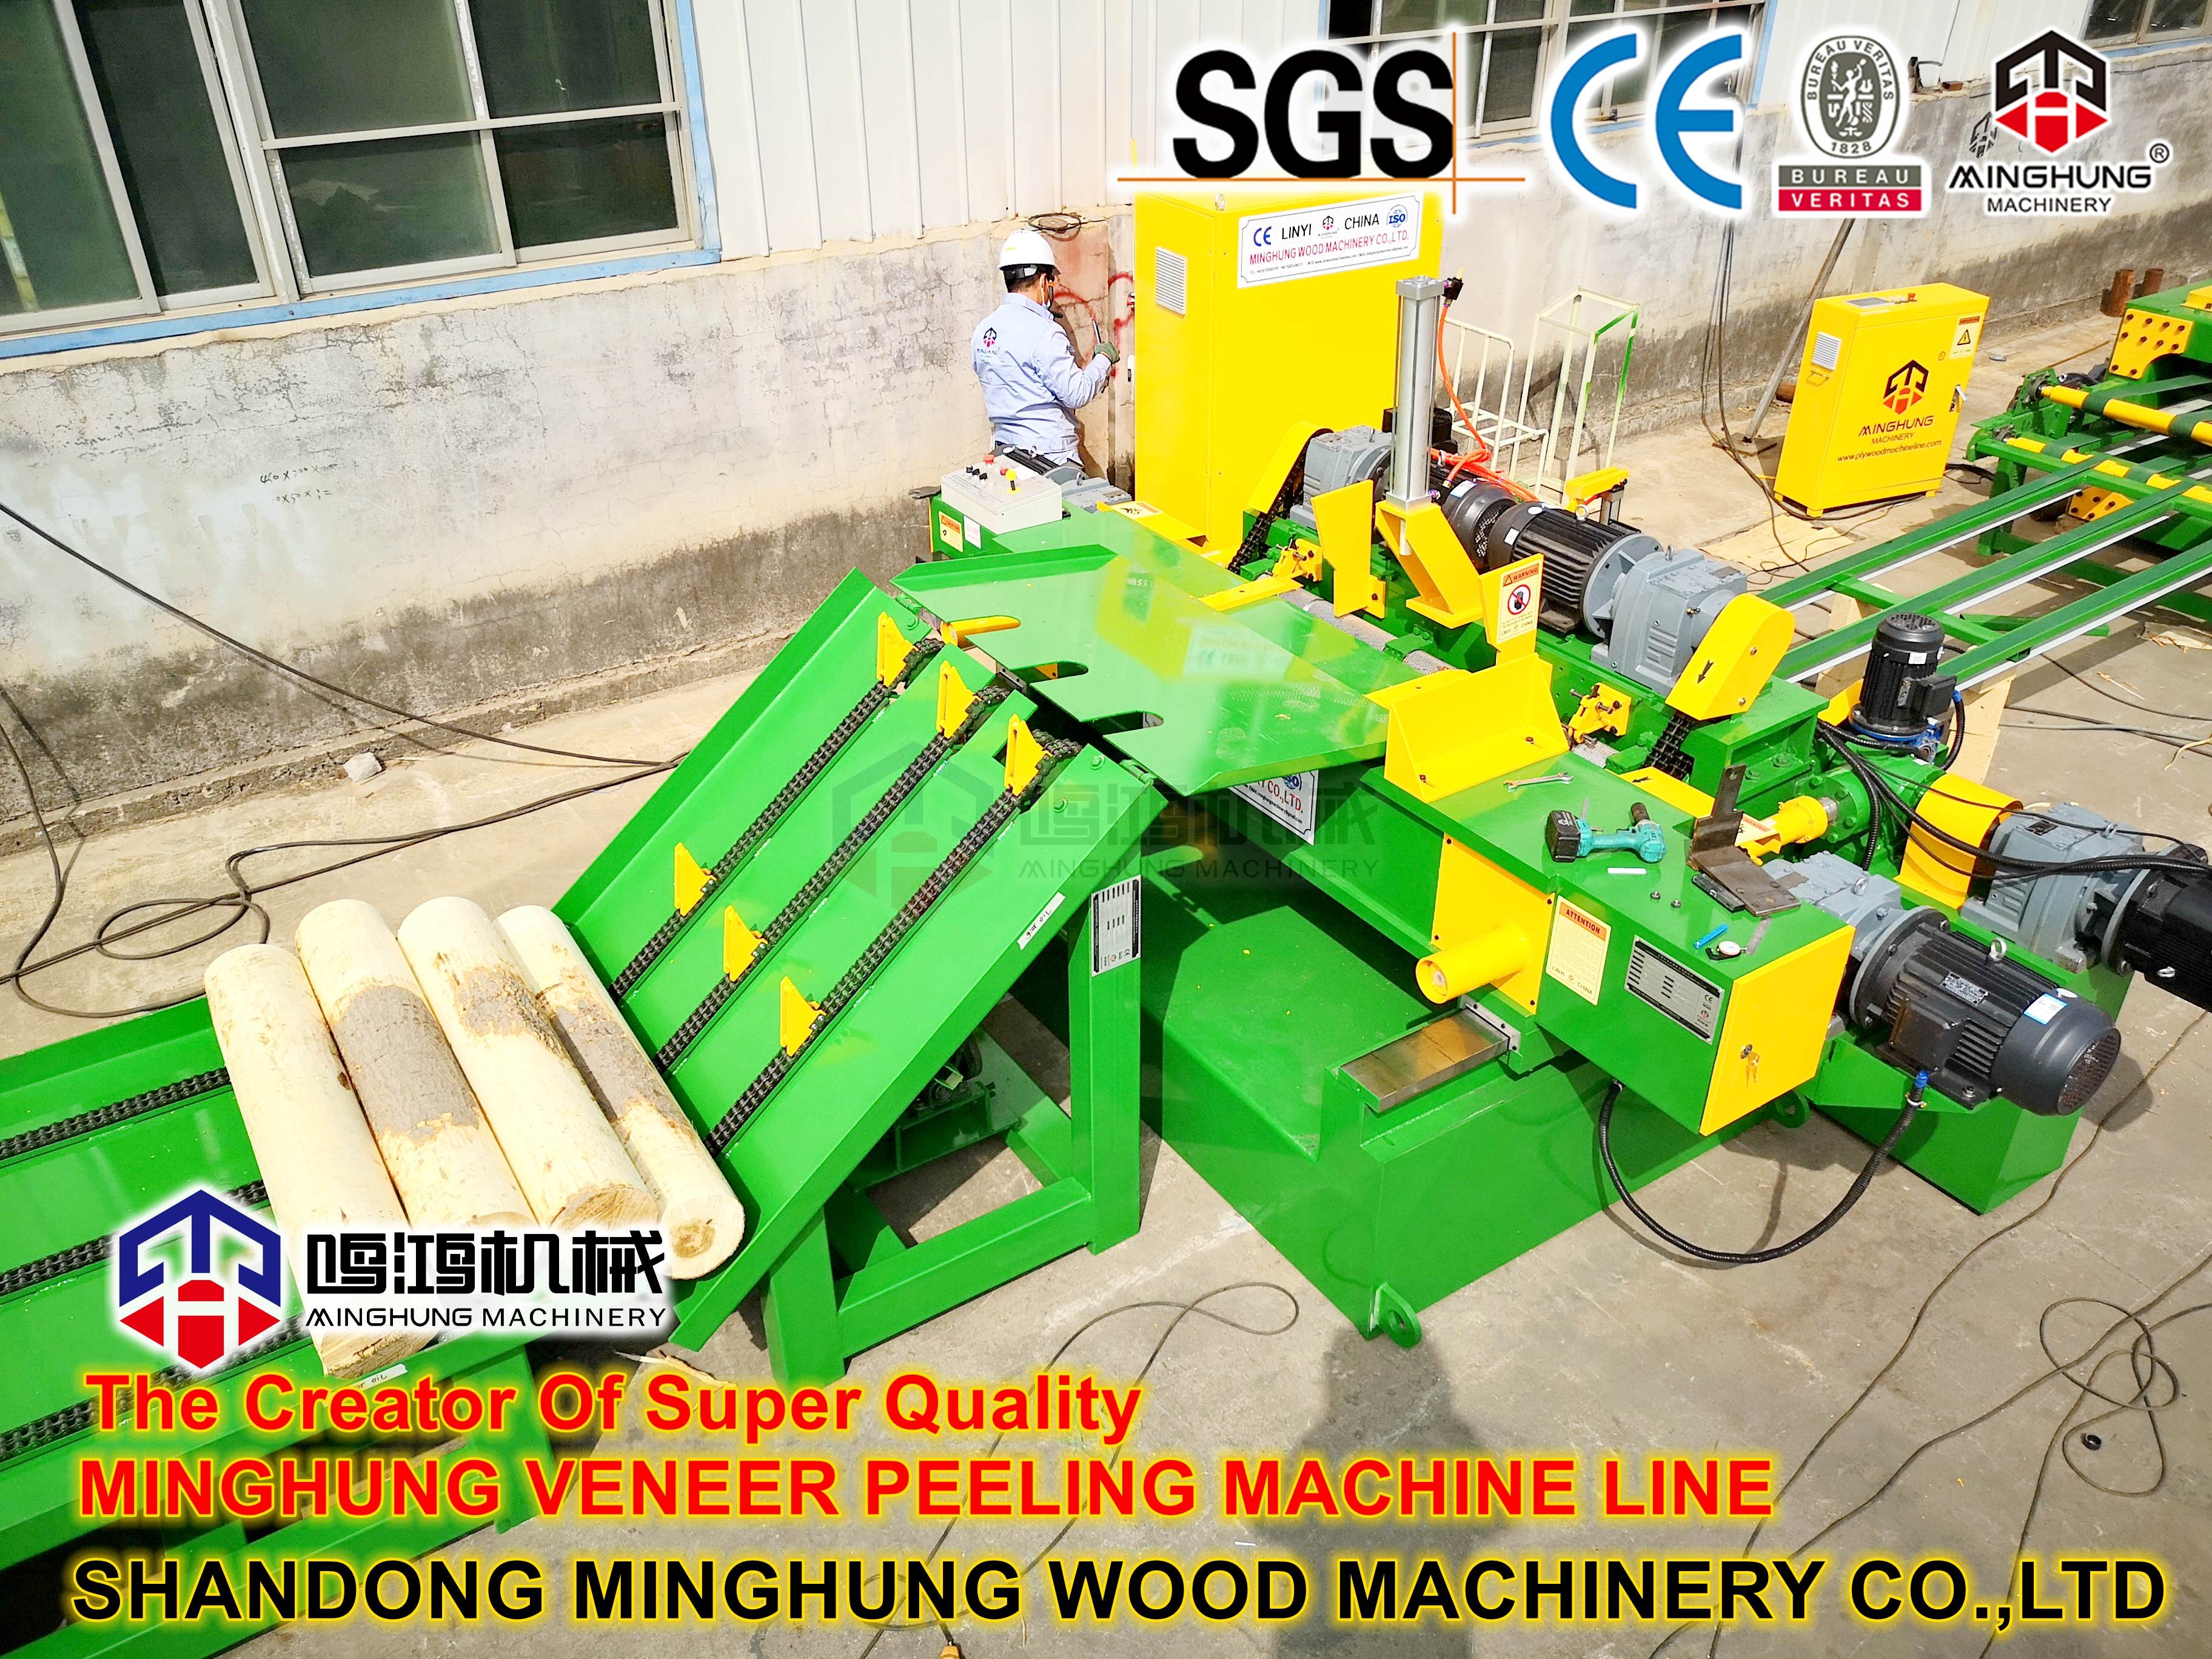
veneer peeling machine
3. Veneer Dryer: Typically roller or mesh belt type, for precise control of veneer moisture content.
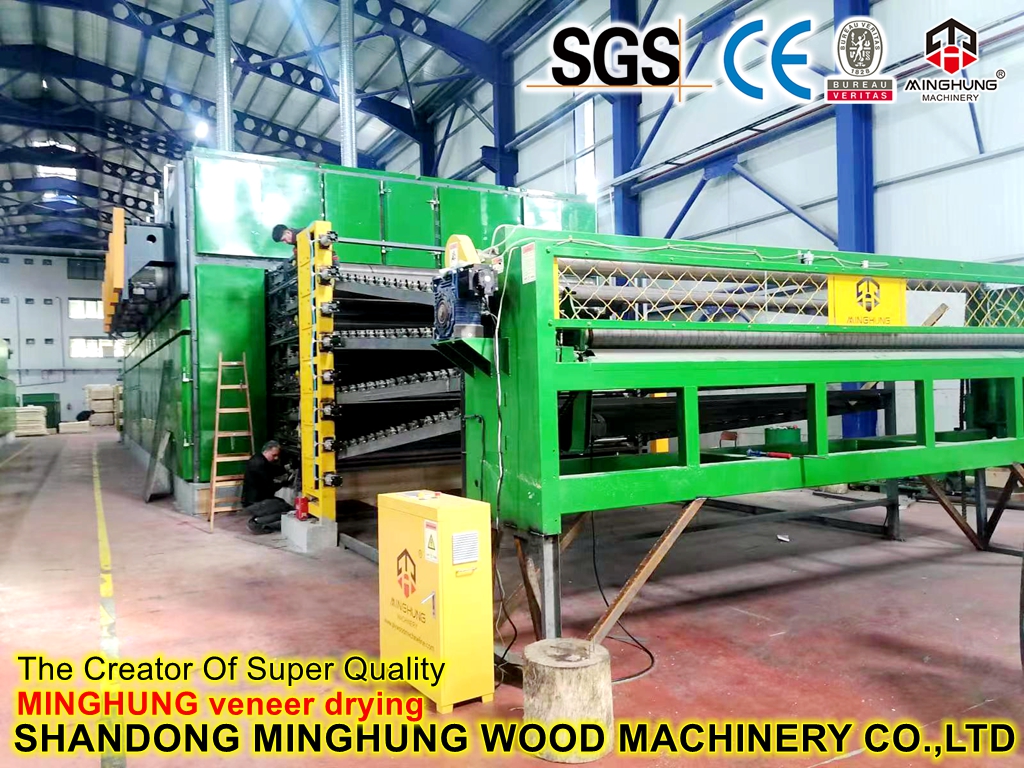
veneer dryer
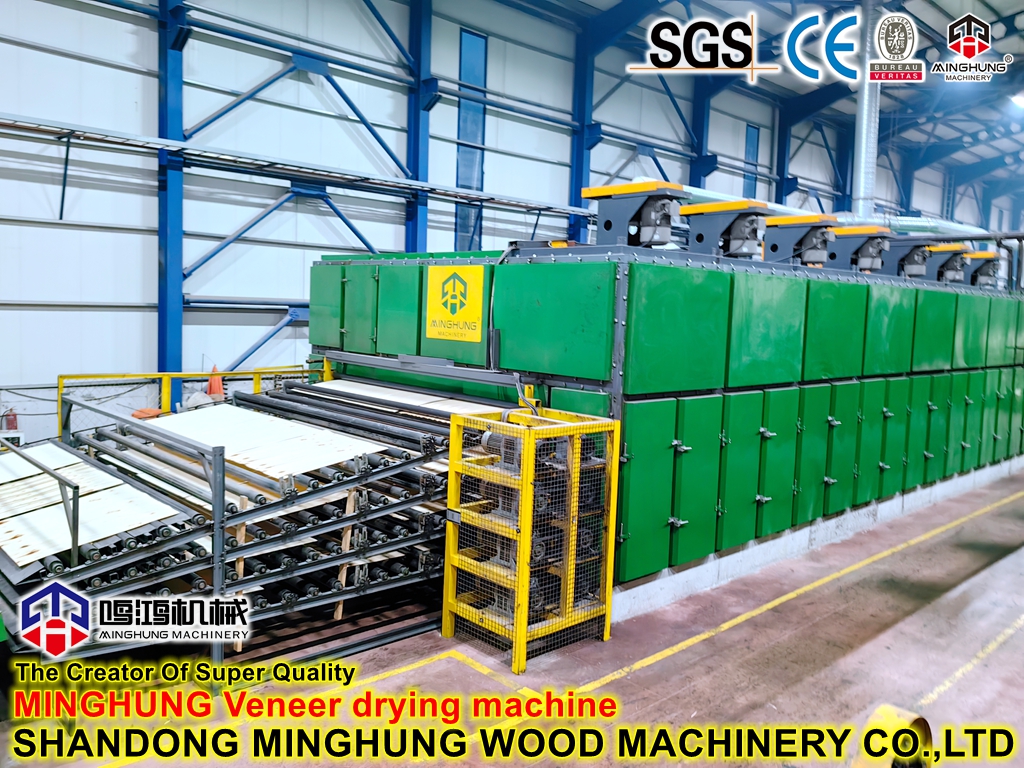
veneer dring machine
4. Formaldehyde-Free Glue Mixing & Application System: A key part of the eco-friendly line, includes Formaldehyde-Free Adhesive Mixing Tanks and the Glue Spreader (can be roller or curtain coater type).
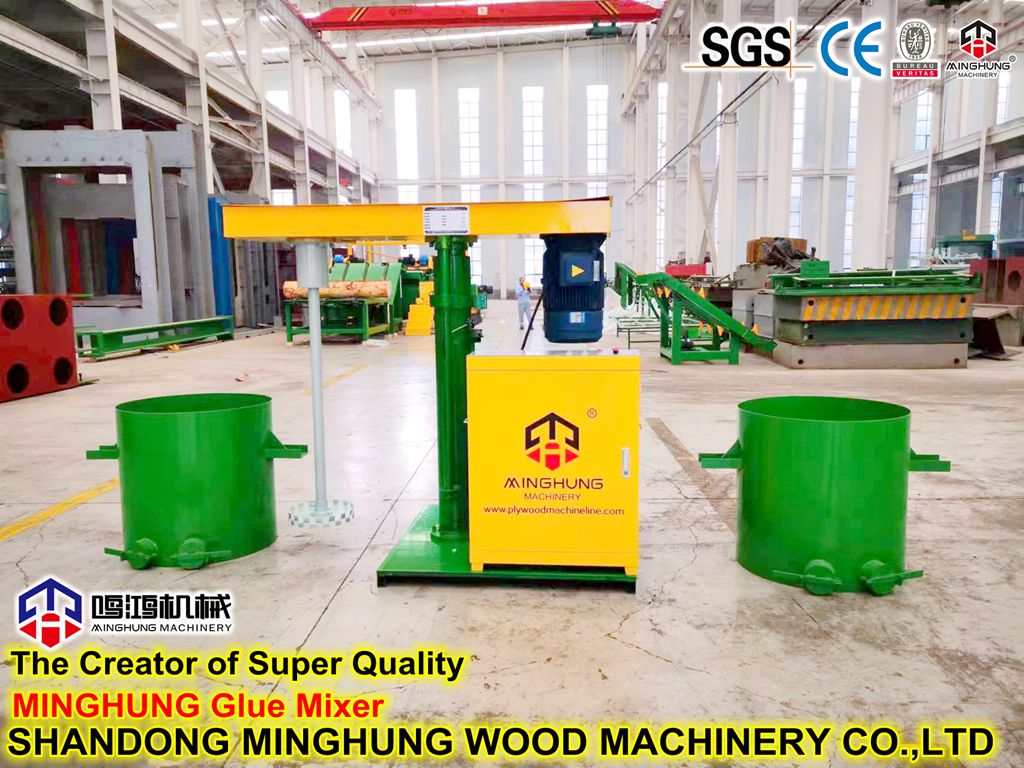
glue mixer
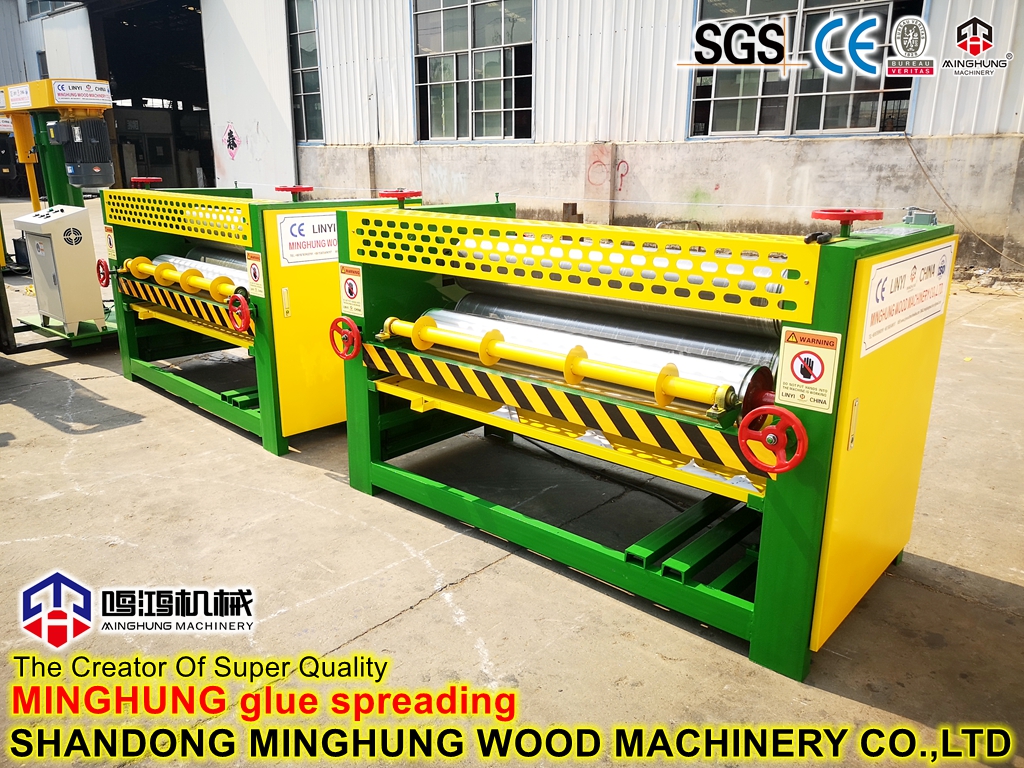
giue spreading machine
5. Automatic Layup Line: Manual layup tables or fully automatic layup machines.
6. Pre-Press: Usually a cold press, for initial mat shaping.
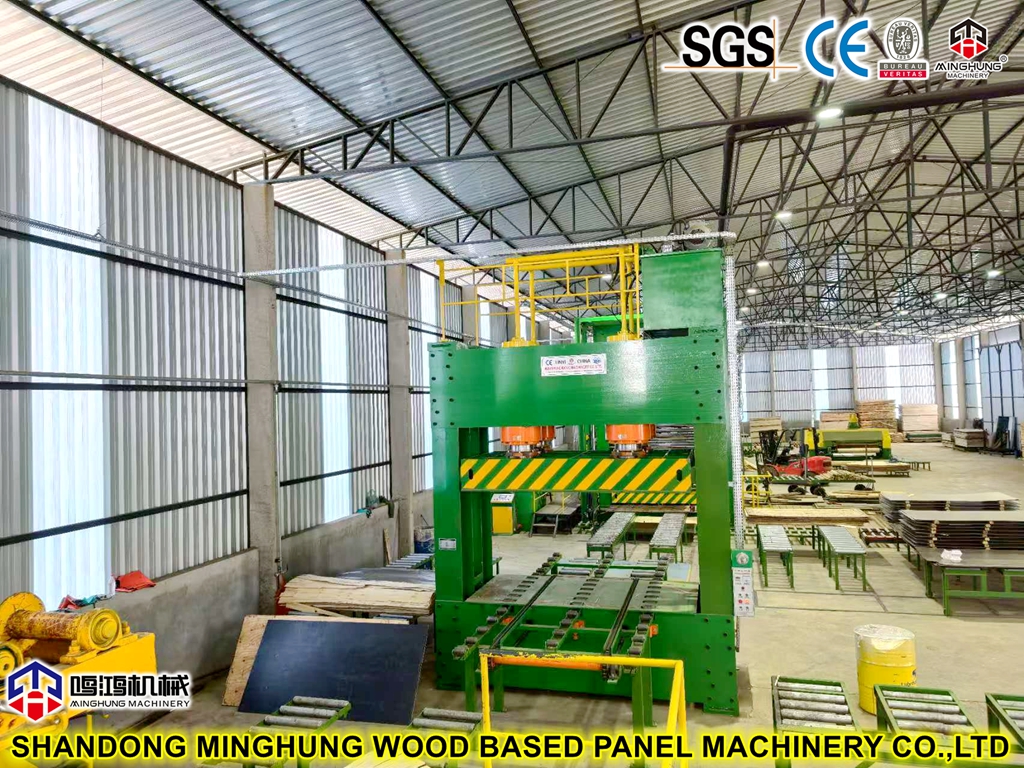
pre pressing machine
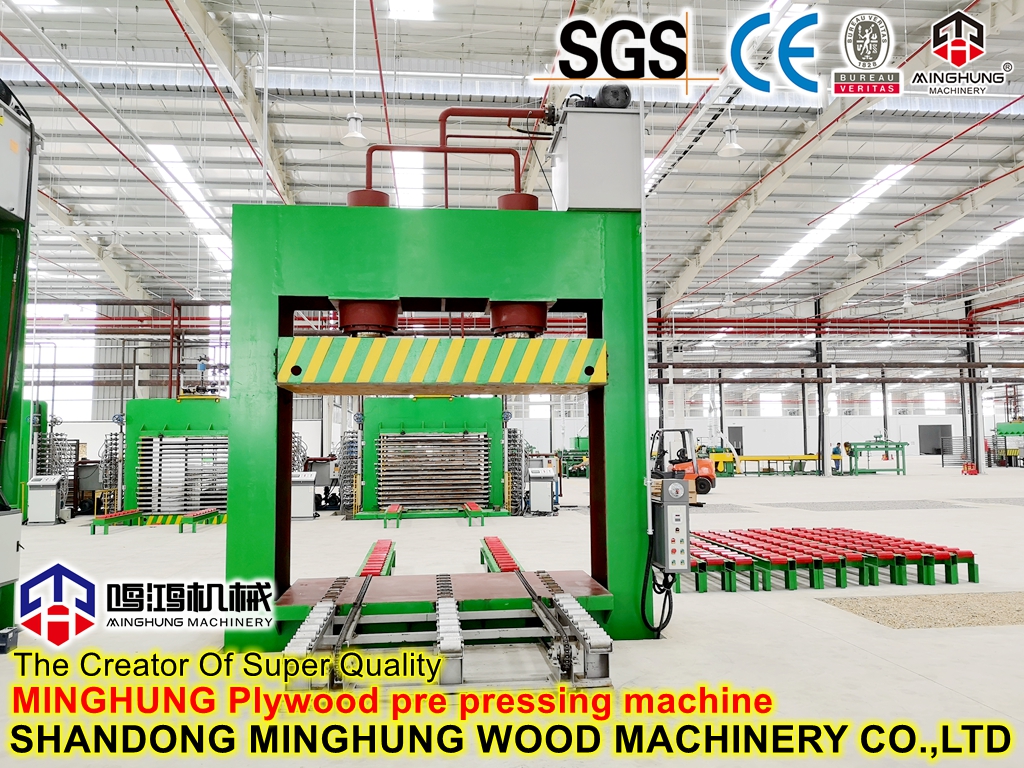
pre press
7. Hot Press: The heart of the production line; a multi-opening hot press or continuous press, providing the heat and pressure for adhesive curing.
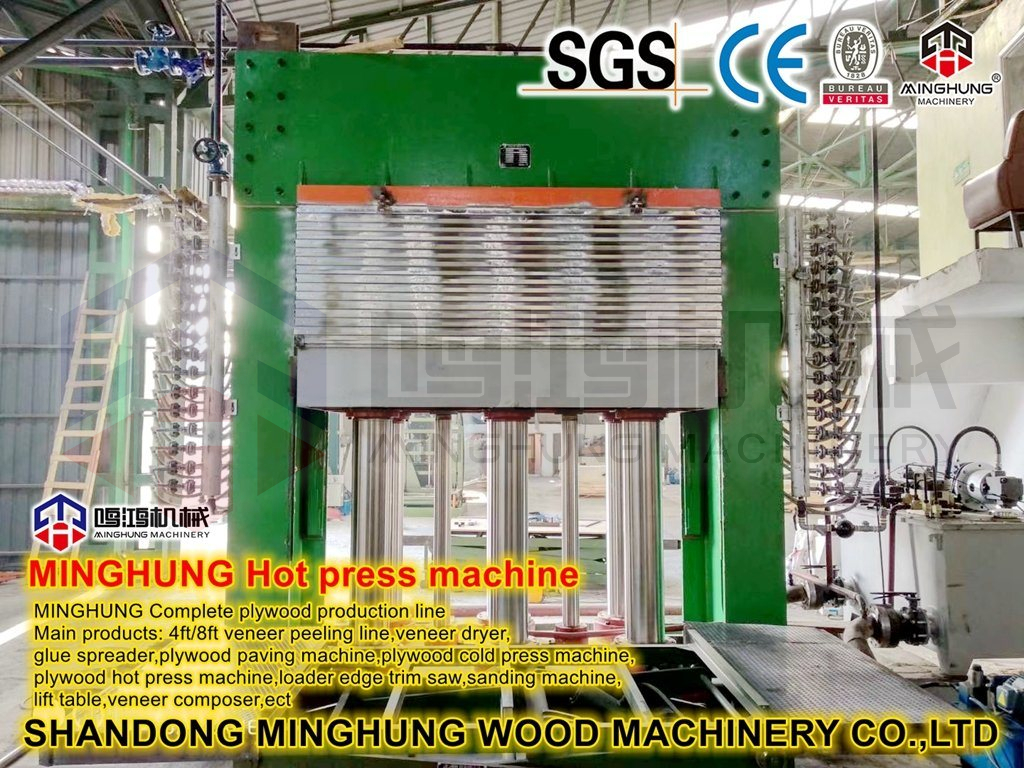
plywood hot press
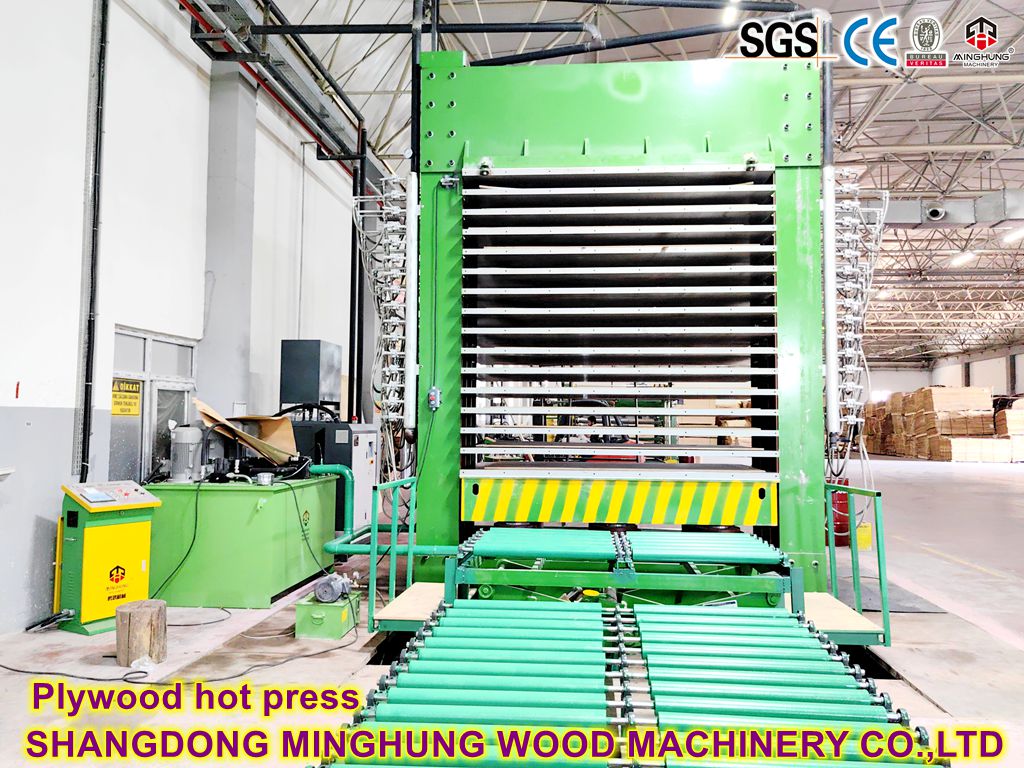
hot press
8. Cooler/Turner: Cools and turns the hot panels after pressing.
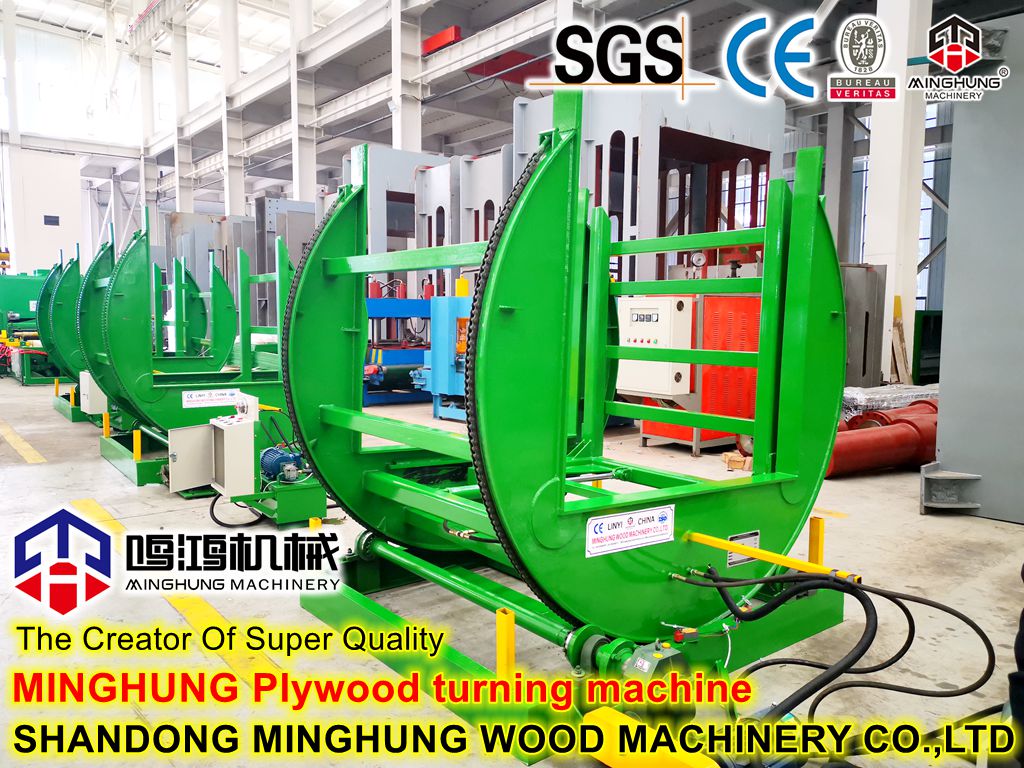
turning machine
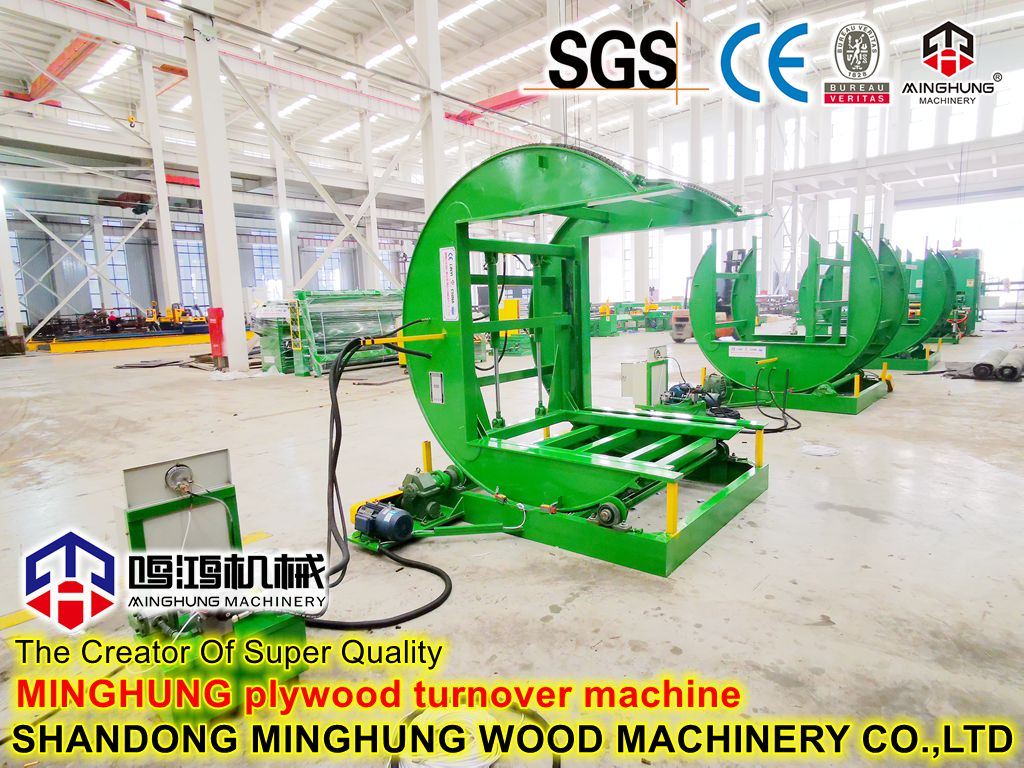
turner
9. Panel Curing (Seasoning) Area: Designated space for panels to rest and release stress.
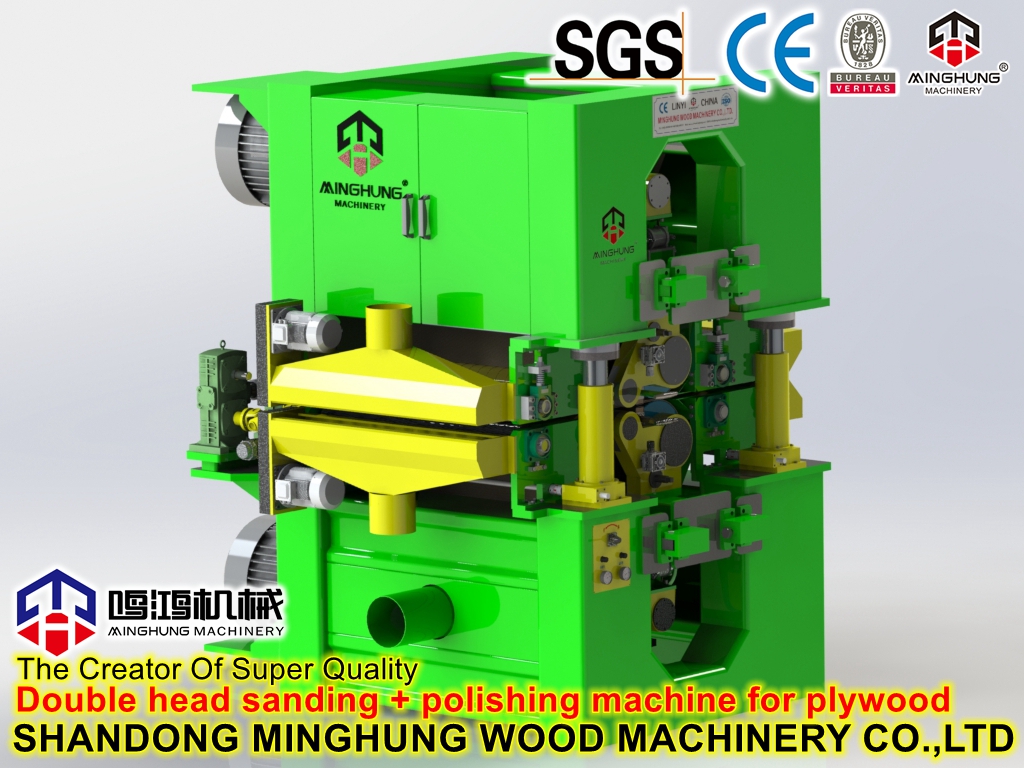
10. Calibrating Sander: Typically a wide-belt sander, for ensuring panel thickness and surface smoothness.
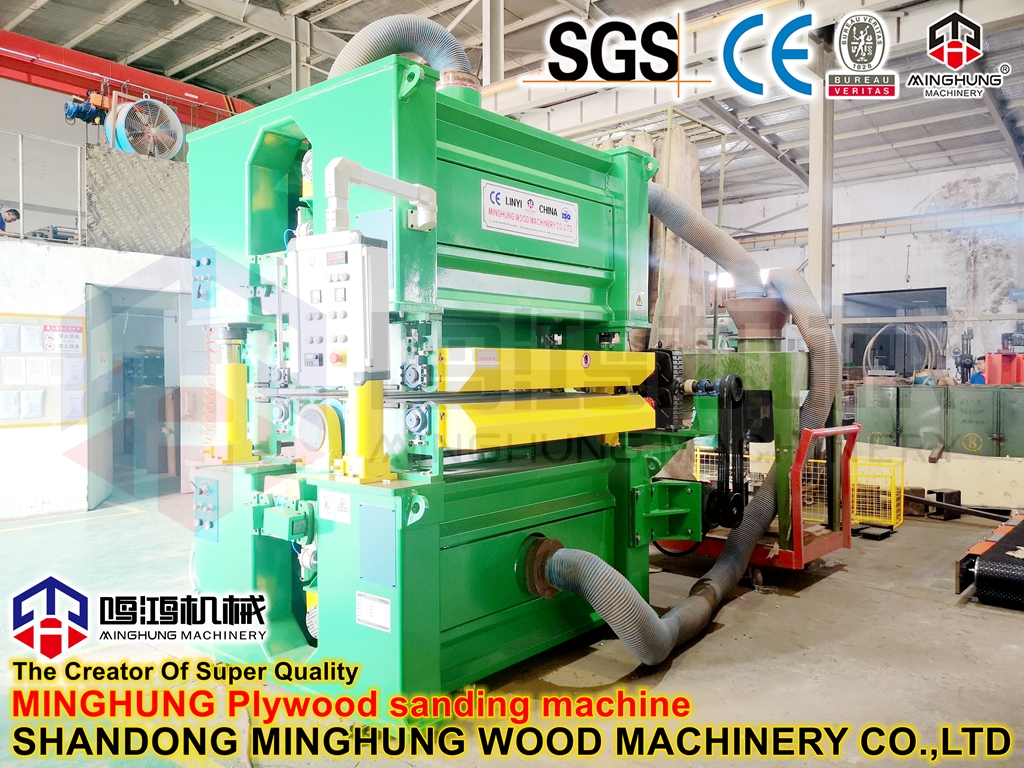
plywood sander
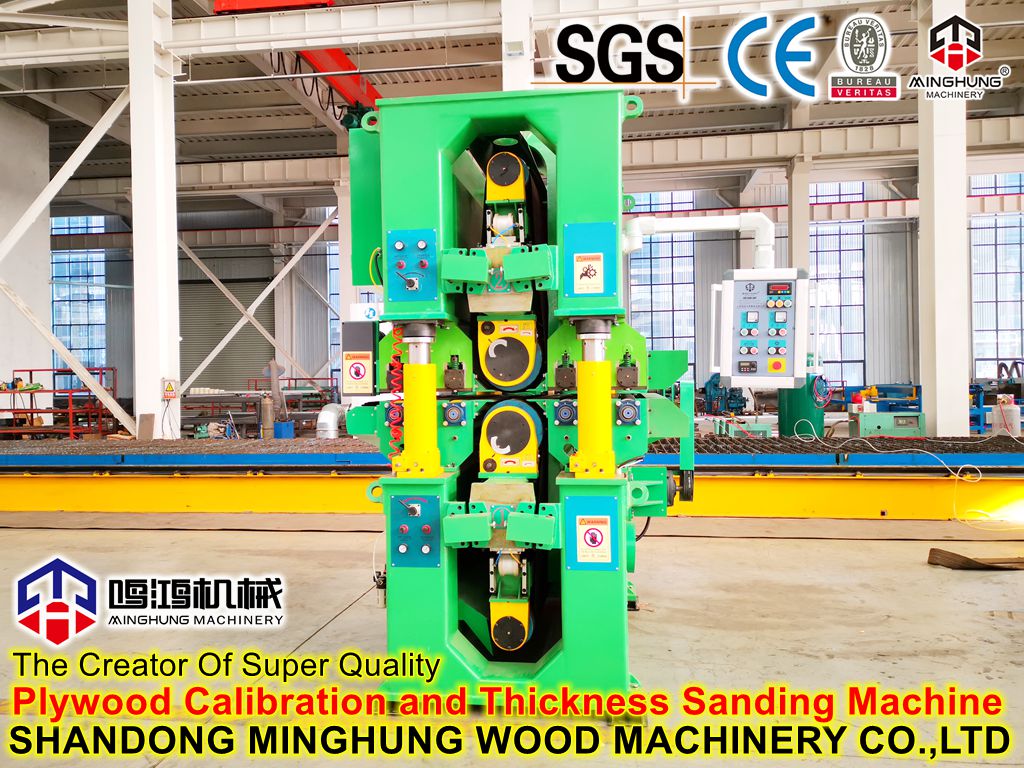
sanding machine
11. Cross-Cutting and Edge-Trimming Saws: For precise trimming of panel length and width.
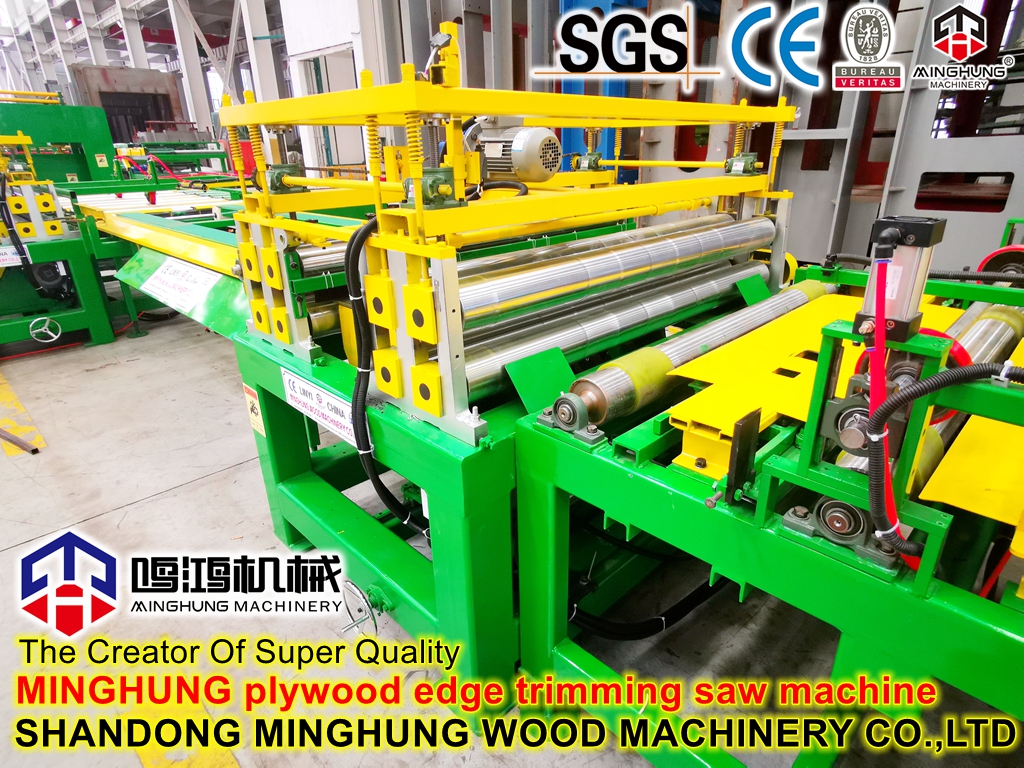
edge trimming machine
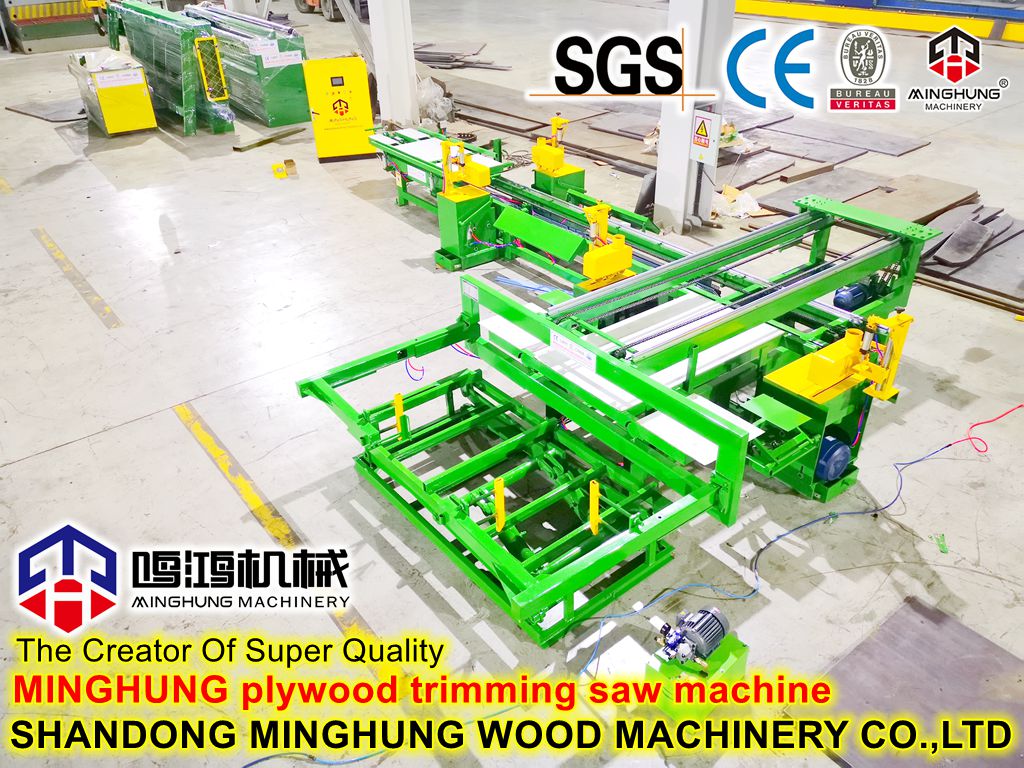
cross cut saw
12. Quality Control Center: Includes inspection tables, measuring tools, and environmental testing equipment.
13. Automatic Stacking and Packaging Machine: For automated stacking and packaging of finished products.
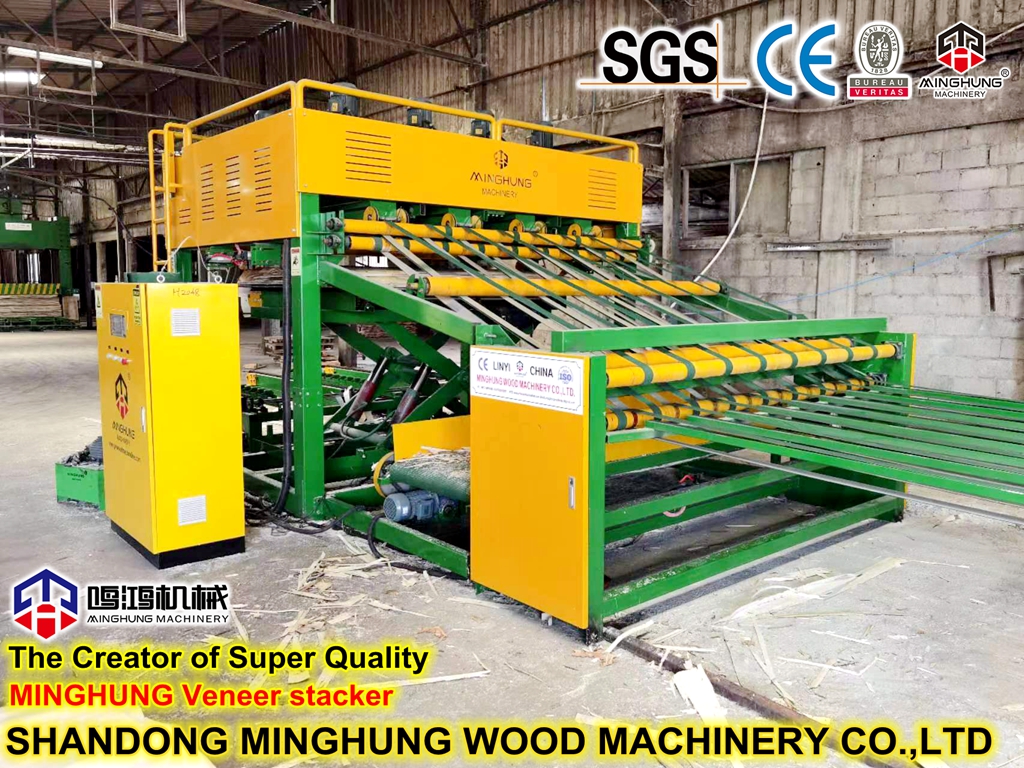
veneer stacker for plywood
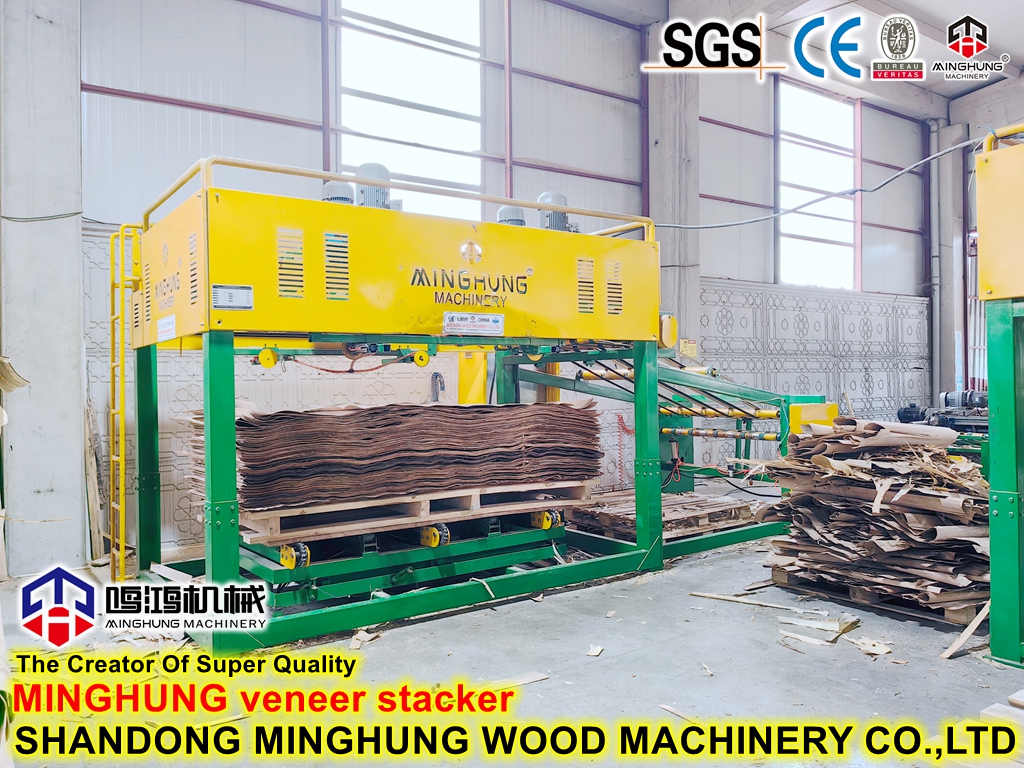
veneer stacker
The production of furniture-grade eco-friendly plywood is a process that deeply integrates "Precision Manufacturing" with "Green Technology." The precise control at every stage, especially the application of formaldehyde-free adhesives and the strict hot-pressing and sanding processes, collectively ensures the final product meets the extreme demands of modern furniture for health, aesthetics, and durability.
|
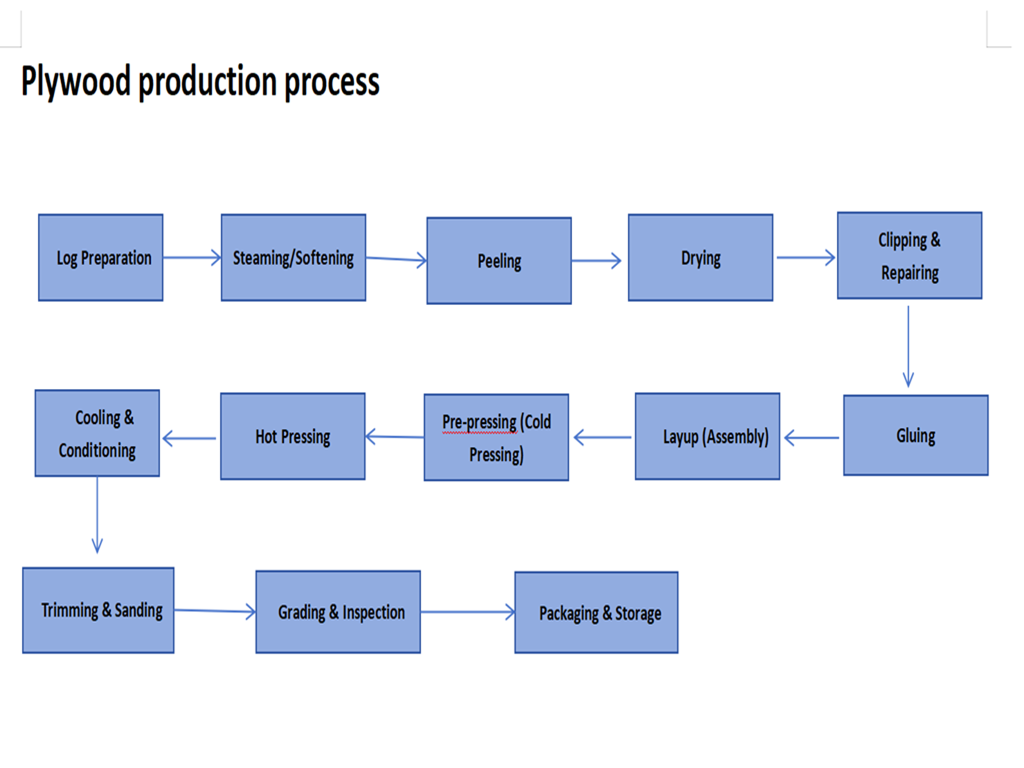
Production Process
The production of furniture-grade eco-friendly plywood is a precise, multi-step process where each stage is crucial to the final product's environmental rating, stability, and aesthetics.
The core process is as follows:
Phase One: Raw Material Preparation & Veneer Processing
1. Log Selection & Treatment
Process: High-quality logs (e.g., Eucalyptus, Poplar, Birch) from sustainably managed forests (e.g., FSC certified) are selected. Logs are cut into specific lengths and softened in a hot water bath to facilitate peeling.
Purpose: To ensure eco-friendly sources and controlled quality of raw materials.
2. Veneer Peeling & Drying
Process: The softened log sections are rotated and peeled on a lathe into continuous, uniform thin sheets called "veneer." The wet veneer is then fed into a dryer to reduce and precisely control its moisture content to a low, uniform level (typically 8%-12%).
Purpose: To create the basic building blocks of plywood. Drying is critical, as high moisture content affects glue adhesion and can cause warping later.
Phase Two: The Eco-Core - Gluing & Layup
3. Formaldehyde-Free Gluing
Process: The dried veneer sheets pass through a Glue Spreader, which applies an even coat of eco-friendly adhesive. For furniture-grade eco-friendly plywood, this involves using formaldehyde-free glues like Soy-Based Adhesive or MDI Adhesive.
Purpose: This is the core step for achieving "eco-friendly" and "formaldehyde-free" status. Using bio-based or MDI adhesives prevents the introduction of formaldehyde at the source.
4. Layup (Assembly)
Process: The glued veneers are assembled manually or automatically following the "symmetry rule" and "odd-number rule." This means the grain direction of adjacent veneers is perpendicular, ensuring balanced strength in all directions.
Purpose: To form the plywood "blank" or "mat," establishing the foundation for its structural stability.
Phase Three: Forming & Curing
5. Pre-Pressing
Process: The assembled mat is first fed into a Pre-Press for initial compaction under cold or slightly warm pressure.
Purpose: To achieve initial bonding between veneers, remove air pockets, and create a tight, handleable mat that can be transported into the hot press.
6. Hot Press Curing
Process: This is the "heart" of the production line. The pre-pressed mat enters a Hot Press subjecting it to high temperature and high pressure. Under specific temperature, pressure, and time settings, the adhesive cures rapidly, permanently bonding the multiple veneer layers into a solid panel.
Purpose: To finalize the panel form and impart the required physical and mechanical strength.
Phase Four: Post-Processing & Quality Control
7. Cooling & Curing (Seasoning)
Process: The newly pressed, hot panels are cooled by a Cooler/Turner. Afterwards, the panels are stored for a period of "curing" or "seasoning."
Purpose: To release internal stress, balance moisture content, stabilize panel performance, and prevent deformation.
8. Calibrating-Sanding & Trimming
Process: The seasoned panels first go through a Calibrating Sander for fine sanding of both surfaces, ensuring precise thickness and a perfectly smooth, flat surface. Then, Cross-Cutting and Edge-Trimming Saws trim the rough edges to achieve exact dimensions and smooth edges.
Purpose: To enhance the panel's appearance and usability, providing a perfect substrate for subsequent finishing processes like laminating or edge-banding.
9. Inspection & Packaging
Process: Finished panels undergo 100% inspection, including thickness measurement, surface defect check, and environmental grade testing (e.g., sampled with formaldehyde detectors). Qualified products are stacked and packaged by an Automatic Stacking and Packaging Machine.
Purpose: To ensure that all shipped products 100% meet the quality and environmental standards for furniture-grade plywood.
|
Comparision with traditional plywood
Feature | Furniture-Grade Eco-Friendly Plywood System | Ordinary Construction/Industrial Plywood |
Environmental Standard | A core indicator. Pursues No Added Formaldehyde (NAF) or ultra-low formaldehyde, with authoritative certifications. | Not a core indicator. Typically meets only E1 or E2 standards; may have a pungent odor. |
Raw Materials | Selected high-quality wood veneers, free of holes and overlaps. | Lower requirements for wood species and veneer quality; may contain mixed wood and have repairs. |
Production Process | Precise glue application, symmetrical layup, strictly controlled hot-pressing curves. | Relatively rough process; higher risk of bonding failure and inconsistency. |
Performance | High strength, high stability, excellent machining performance. | Average performance, prone to warping, and susceptible to chipping during machining. |
Appearance | Smooth surface, clear grain, suitable for direct veneering or painting. | Rough surface, often used as a substrate that will be covered. |
Primary Use | High-end furniture, interior decoration, children's rooms, commercial spaces. | Formwork, packing cases, partitions, and other non-exposed structures. |
|
Main application scenarios
High-End Custom Furniture: Wardrobes, bookshelves, TV cabinets, dining tables, etc.
Children & Infant Furniture: The sector with the highest requirements for environmental protection and safety.
Kitchen & Bathroom Cabinetry: Especially the moisture-resistant product series.
Hotel & Commercial Fixed Furniture: Such as wall cladding, fixed partitions, reception desks, etc.
Interior Doors & Door Frames: Ensures no warping or cracking.
Artwork or Decorative Components requiring intricate carving and laser cutting.
We can offer factory layout design, installation, operator training, 24-month warranty, and global spare parts delivery within 72 hours.
Whatsapp: +8618769900191 +8615589105786 +8618954906501
Email: osbmdfmachinery@gmail.com